· Updated - TITANIUM 3DP Engineering - Engineering Guides - 15 min read
Titanium 3D Printing for Battery Recycling and Critical Minerals Processing Parts
Engineering RFQ guide for titanium 3D printed battery recycling and critical minerals processing parts, covering black mass leach loops, manifolds, CP titanium, corrosion exposure, leak testing, CT, CMM, and traceability.
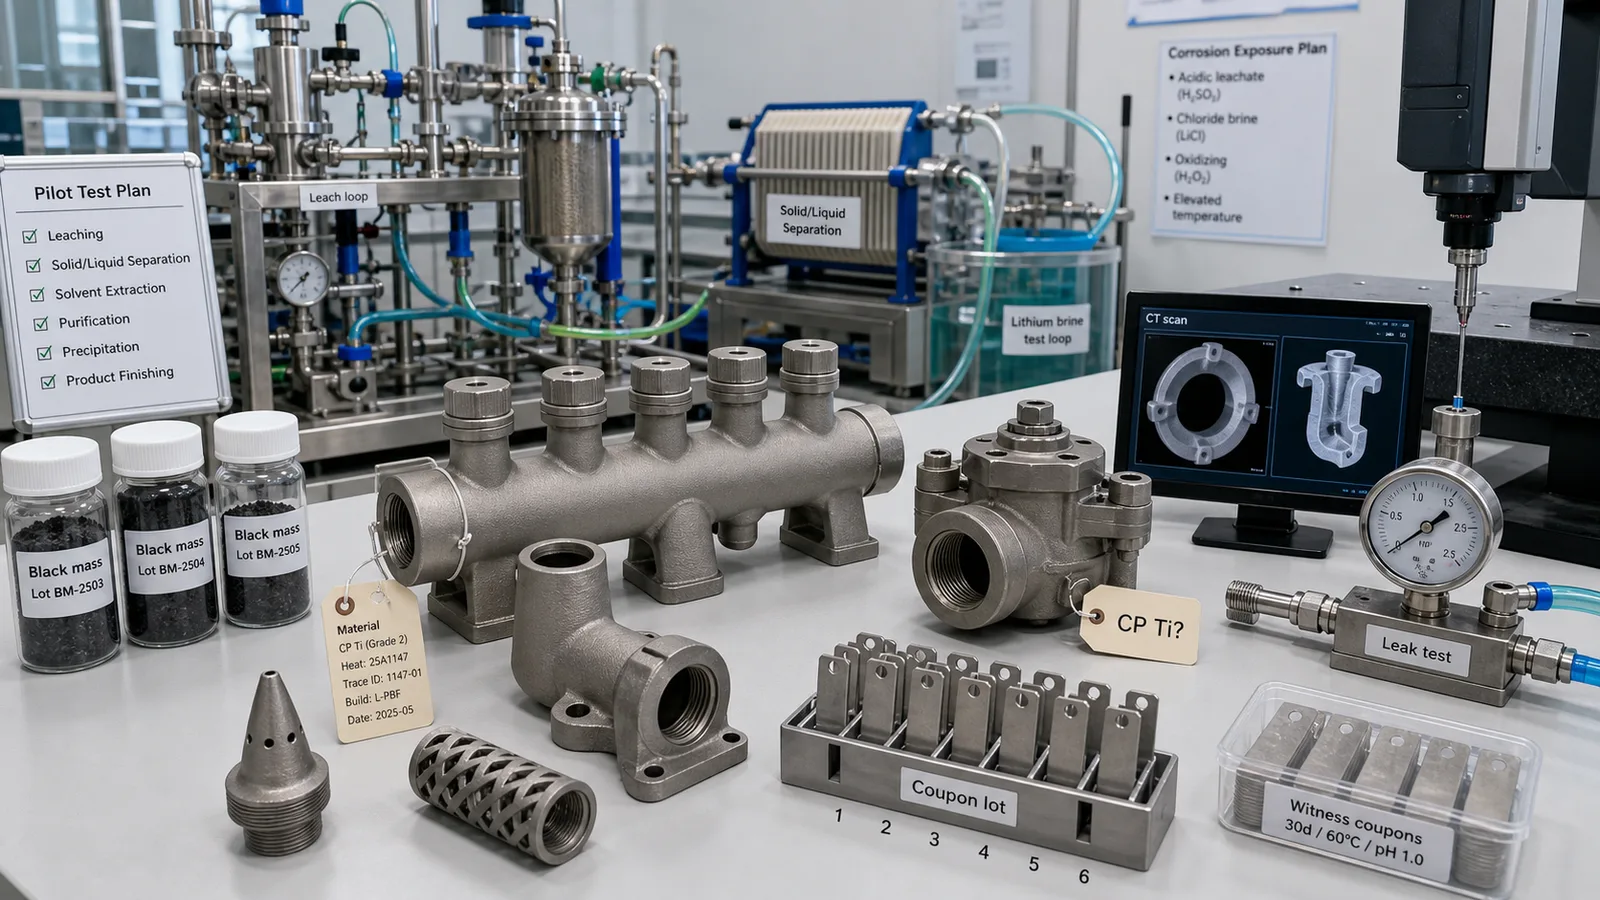
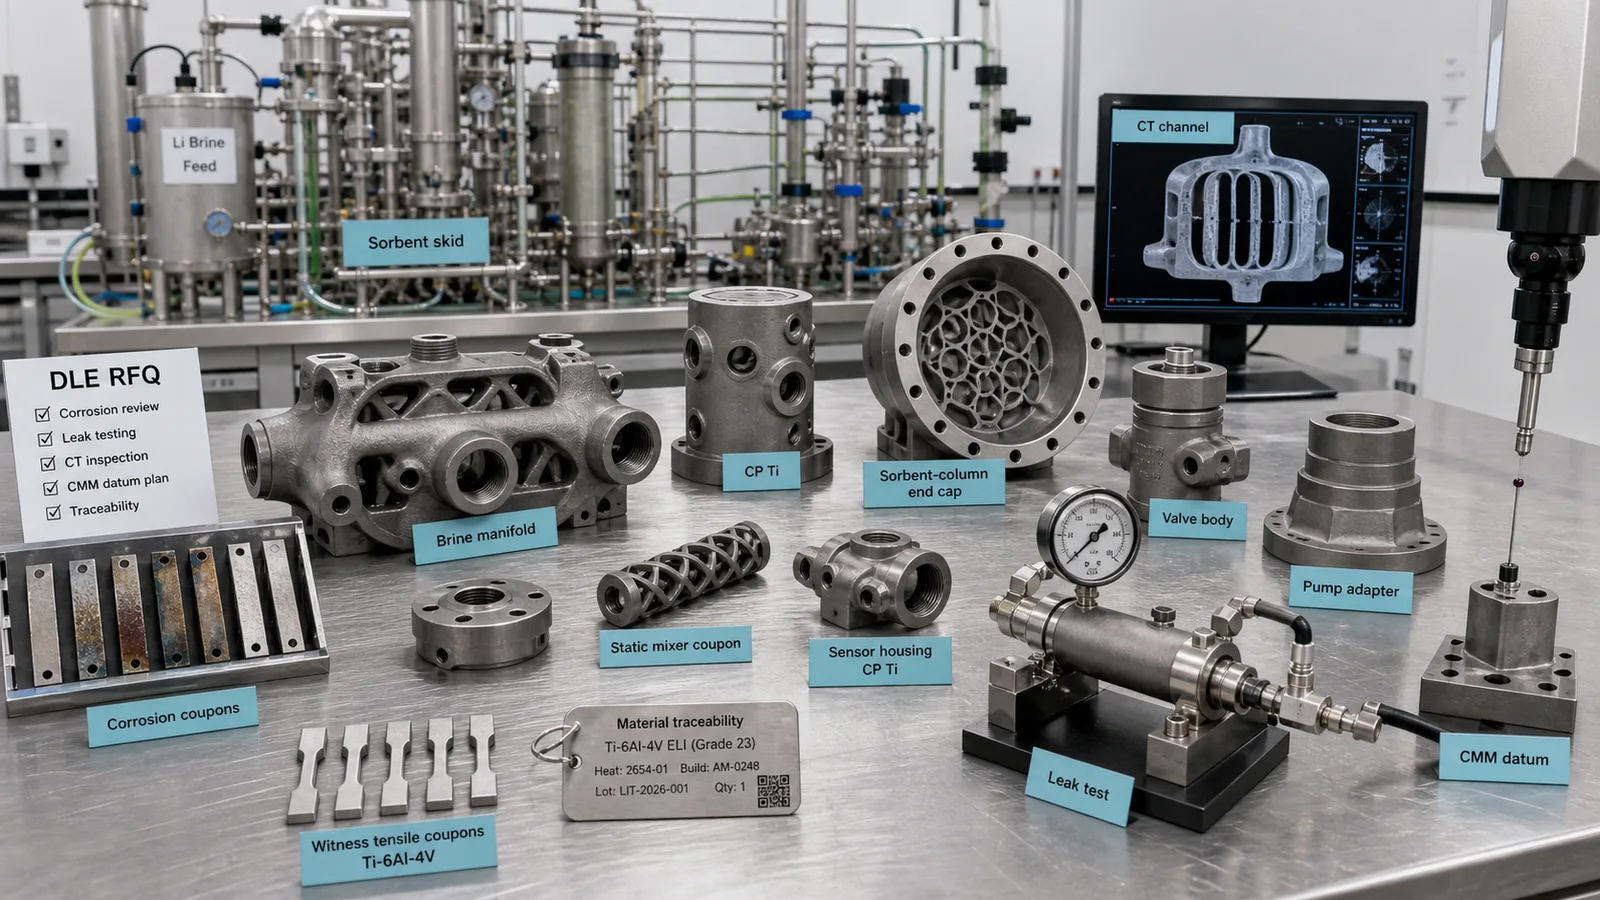
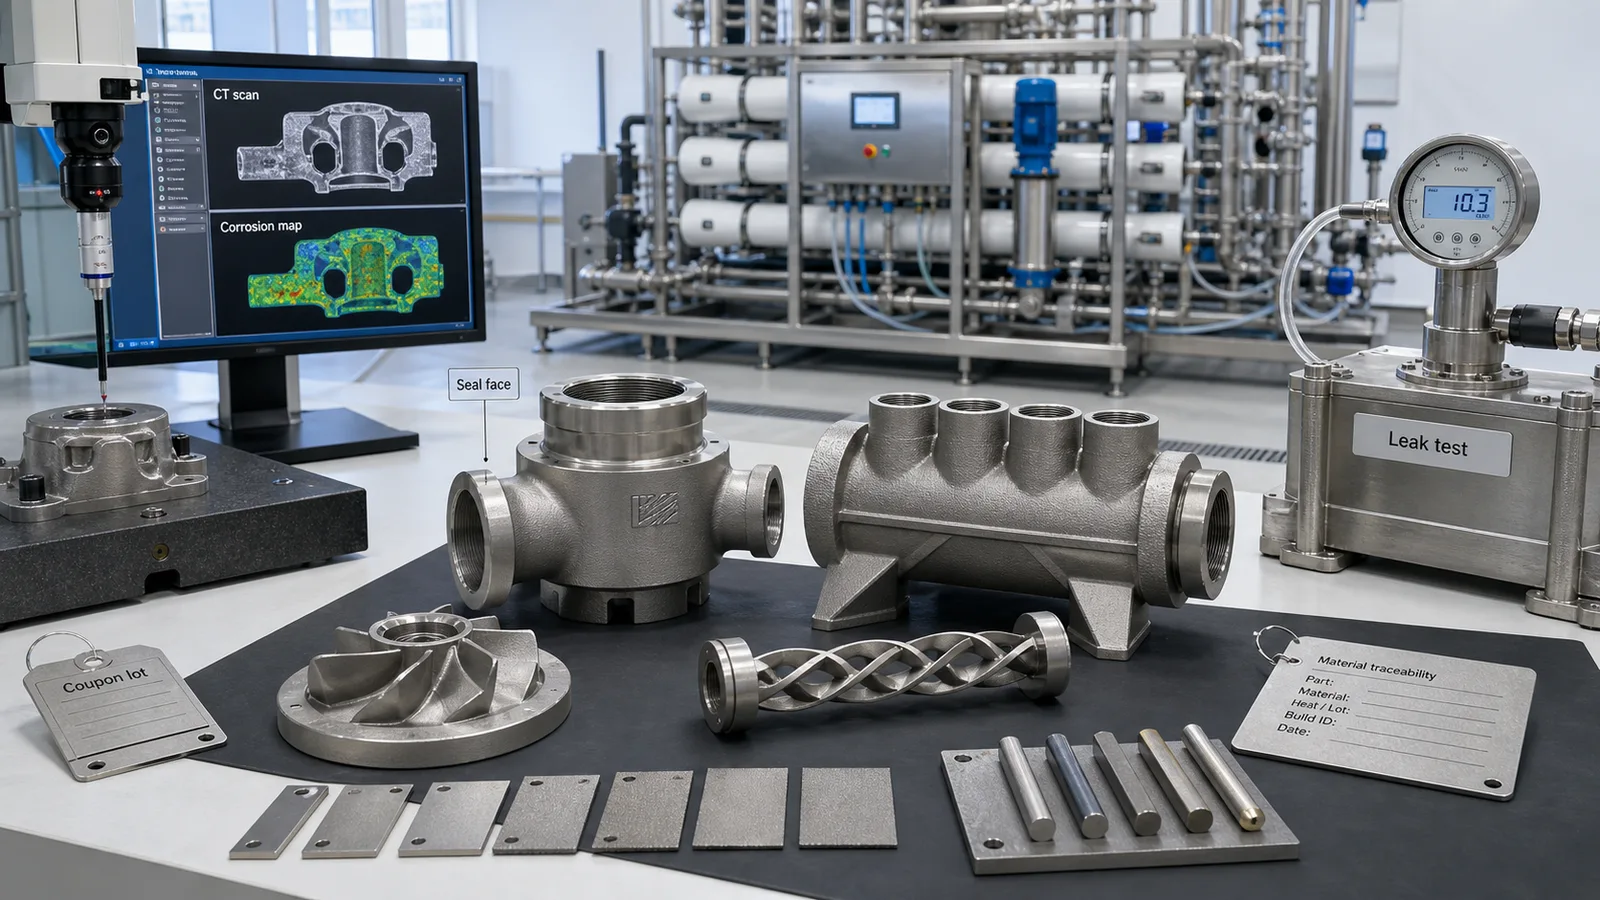
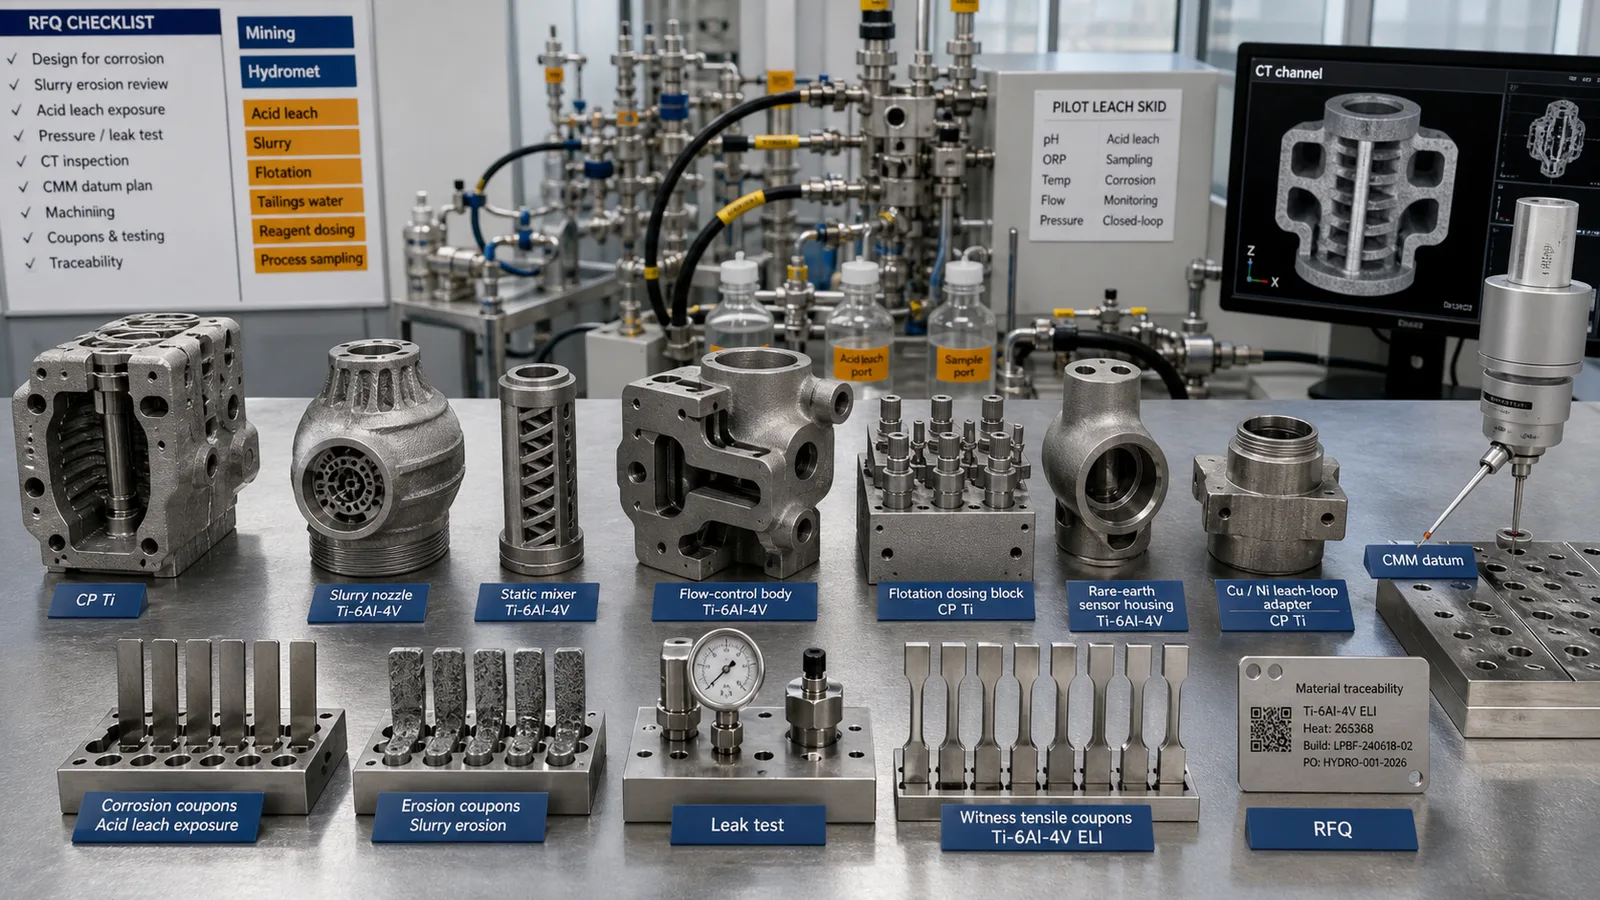
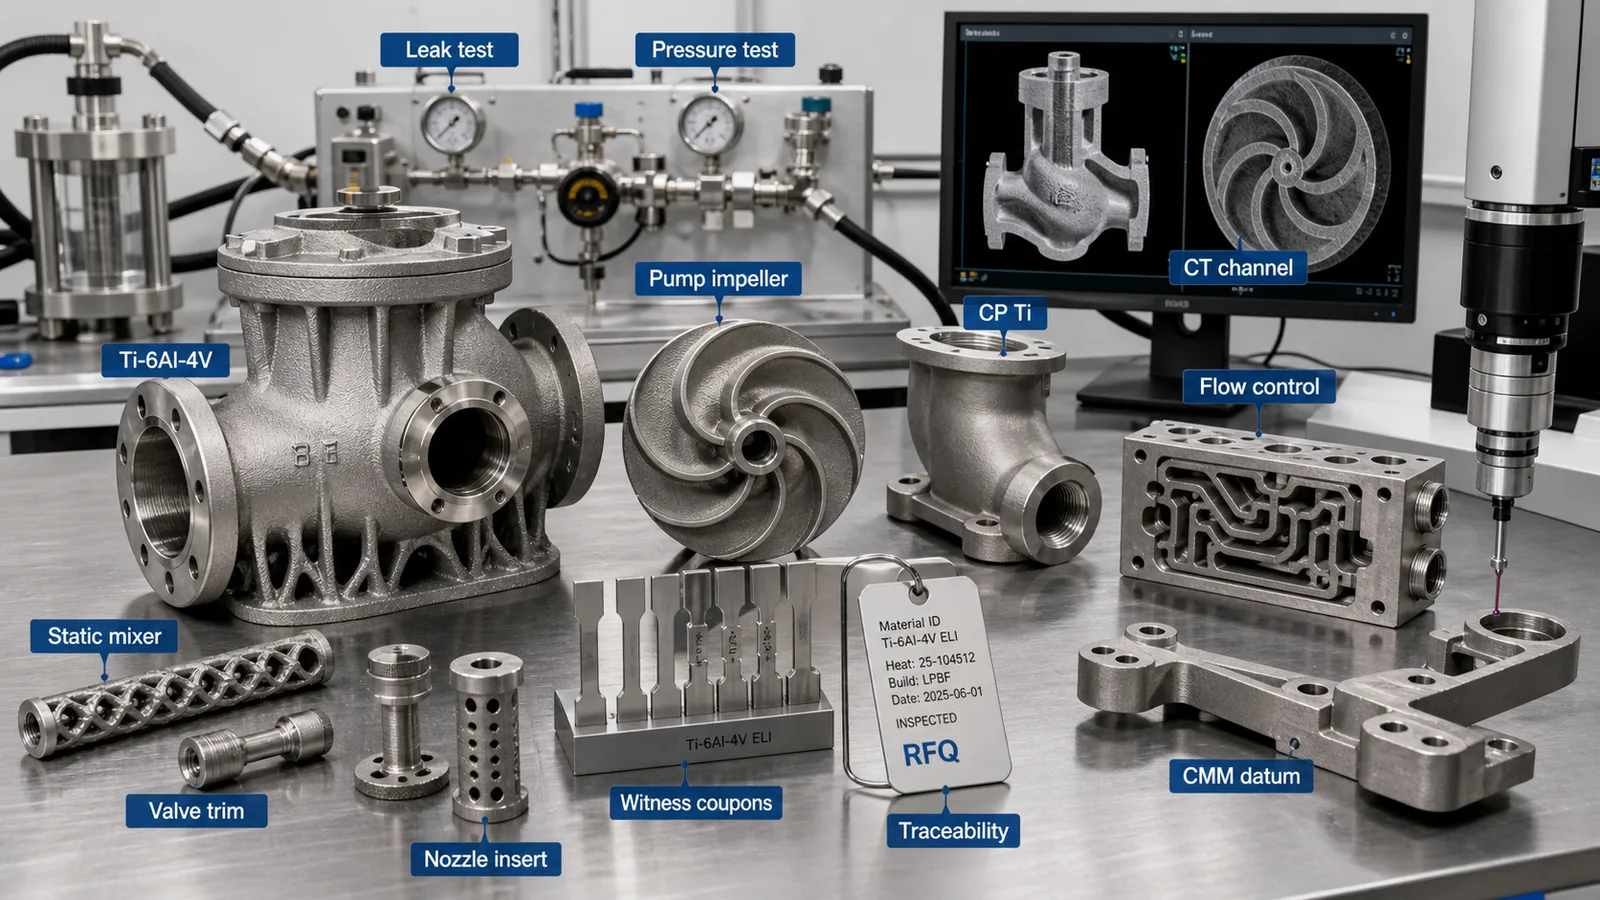
Representative article image; not a customer acceptance record or proof of a qualified manufacturing route. Refer to the cited sources and part-specific inspection records for engineering evidence.
On this page
Titanium 3D printing for battery recycling and critical minerals processing parts is useful when corrosive process fluids, compact pilot hardware, low-volume iteration, fewer leak paths, or difficult internal flow geometry creates a real engineering advantage. It is not a generic substitute for tanks, pipe spools, catalog valves, lined equipment, or commodity stainless process hardware.
The strongest RFQs treat a printed titanium manifold, leach-loop adapter, dosing nozzle, static mixer, pump adapter, sample block, corrosion coupon rack, or lithium brine test fixture as delivered process hardware. That means the quote must cover exposure mapping, alloy choice, seal faces, cleaning, pressure or leak testing, CT when hidden channels matter, CMM, material records, and traceability.
For the broader process-equipment context, start with Titanium 3D Printing for Chemical Processing and Water Treatment Parts and use this guide for battery recycling and critical-minerals-specific decisions. For pump adapters, valve bodies, static mixers, nozzles, and cross-industry flow-control hardware, use Titanium 3D Printing for Industrial Valves, Pump Parts, and Flow Control Hardware. For DLE brine manifolds, sorbent-column hardware, and lithium brine pilot skids, use Titanium 3D Printing for Direct Lithium Extraction and Brine Processing Hardware. For primary mining, mineral processing, acid leach, slurry, flotation, and broader hydrometallurgy pilot hardware outside battery recycling, use Titanium 3D Printing for Mining, Mineral Processing, and Hydrometallurgy Hardware.
Quick Answer
Titanium additive manufacturing is worth reviewing for battery recycling and critical minerals processing when the part is compact, corrosion-exposed, prototype-heavy, interface-dense, or improved by internal routing that conventional machining cannot deliver efficiently.
Good candidates include:
- Black mass leach-loop manifolds, sample blocks, and sensor-port bodies for pilot systems.
- Corrosion-resistant dosing nozzles, static mixer inserts, and reagent injection adapters.
- Pump adapters, valve bodies, filter adapters, and solid-liquid separation test hardware.
- Lithium brine, direct lithium extraction, or ion-exchange test fixtures where corrosion and low-volume iteration matter.
- Coupon racks and exposure fixtures for comparing CP titanium, Ti-6Al-4V, stainless, nickel alloy, polymers, or lined hardware.
- CT-inspected internal-channel samples used to validate depowdering and cleaning before larger process hardware.
- Lab and pilot-line parts that integrate ports, drain paths, pressure taps, and machined seal faces.
Weak candidates include large tanks, pipe runs, simple plates, commodity fittings, high-volume molded or cast parts, and any wetted part where the RFQ does not define chemistry, temperature, pressure, solids, cleaning route, seal faces, proof test, and documentation.
If a machined block, lined steel part, polymer component, stainless fabrication, nickel alloy, conventional titanium fabrication, or catalog process component meets the chemistry, cost, lead-time, and evidence requirements with lower risk, use the When Not to Use Titanium Additive Manufacturing screen before requesting production pricing.
Why This Topic Is Timely in 2026
Specify where the component sits in the recycling route before discussing titanium AM: black-mass slurry handling, leach sampling, reagent dosing, washing, and clean-solution measurement impose different conditions. Solids, cleaning residues, cross-contamination, and replaceable wear features should be resolved alongside chemical exposure.
Recent public signals show the context:
- The IEA Global Critical Minerals Outlook 2025 reported that lithium demand rose by nearly 30% in 2024, while nickel, cobalt, graphite, and rare earth demand also increased. For battery metals such as lithium, nickel, cobalt, and graphite, the energy sector accounted for most recent demand growth.
- The IEA’s 2025 outlook notes that scaling recycling can reduce the need for new mining activity and that recycled energy-transition minerals can have materially lower greenhouse gas emissions than primary mined materials.
- In April 2026, the IEA reported that battery recycling innovation is surging as countries work to strengthen critical mineral supply and energy security.
- DOE’s Critical Materials overview highlights battery manufacturing and recycling grants, battery material processing grants, and research focused on recycling and better use of critical materials.
- DOE’s Lithium-Ion Battery Recycling Prize and ReCell-related work show continued attention to collection, recycling, and reuse of lithium-ion battery materials.
- EPA’s Lithium-Ion Battery Recycling page describes hydrometallurgy as a liquid-based leaching route for recovering metals from black mass, while direct recycling preserves the cathode structure; both paths create different hardware assumptions for leaching, separation, purification, precipitation, cleaning, and evidence.
These signals do not mean every recycling or mineral-processing part should be printed in titanium. They explain why more teams are asking sharper RFQ questions about corrosion-resistant pilot hardware, compact test loops, leak paths, cleanability, and documented material condition.
Where Titanium AM Fits in Battery Recycling Hardware
Battery recycling and critical minerals processing include many steps: collection, discharge, dismantling, shredding, sorting, black mass handling, leaching, solid-liquid separation, solvent extraction, precipitation, purification, washing, drying, and product finishing. Titanium AM only fits selected points in that process chain.
| Part family | Why titanium AM can help | Main RFQ risk | Evidence to define |
|---|---|---|---|
| Leach-loop manifold | Compact routing, fewer fittings, sensor integration | Acid exposure and trapped solids | Exposure map, cleaning route, pressure test |
| Dosing nozzle or reagent adapter | Custom injection geometry and corrosion resistance | Blockage and erosion | Flow test, roughness, material choice |
| Static mixer insert | Internal geometry that is hard to machine | Powder removal and cleanability | CT or flow check, depowdering route |
| Pump or valve adapter | Low-volume interface hardware | Seal faces and threaded ports | Machined faces, CMM, leak test |
| Lithium brine test body | Corrosion-resistant pilot hardware | Chloride and scaling assumptions | Fluid chemistry, coupon evidence |
| Coupon rack | Exposure comparison and material screening | Over-specifying a simple holder | Alloy, finish, coupon lot records |
| Filter or separation adapter | Integrated ports and compact test setup | Solids collection and cleaning | Drain path, cleaning access, inspection photos |
The best candidates are not generic “battery recycling parts.” They are compact process components where additive geometry reduces fittings, integrates sampling or sensor features, shortens pilot-line iteration, or makes a cleanable corrosion-resistant flow path practical.
For heat-transfer or wash-fluid hardware, pair this with Titanium 3D Printed Heat Exchangers. For AI and electronics cooling loops that may share coolant compatibility concerns, see Titanium 3D Printing for AI Data Center Liquid Cooling Hardware.
Start With the Exposure Map
“Battery recycling service” is not a material requirement. A black mass slurry, acidic leachate, chloride brine, sulfate solution, peroxide-containing oxidizing solution, solvent extraction stream, alkaline wash, and deionized-water rinse can all create different material and cleaning assumptions.
Define:
- Process step: leaching, filtration, solid-liquid separation, solvent extraction, purification, precipitation, washing, or test-loop duty.
- Fluid chemistry: acid, base, chloride, sulfate, fluoride, oxidizer, solvent, chelator, inhibitor, or rinse water if known.
- Solids: black mass, graphite, metal foil, scale, precipitate, filter cake, or abrasive particles.
- Temperature, pressure, flow rate, solids loading, pH, concentration, and duty cycle.
- Stagnation, drainability, cleaning, flushing, and maintenance intervals.
- Mating materials: stainless, duplex stainless, nickel alloy, polymers, fluoropolymers, elastomers, lined steel, graphite, or glass.
- Whether the part is a prototype, pilot-plant component, reliability-test article, or production-intent part.
- Acceptance tests: leak, pressure hold, flow, cleaning verification, roughness, CMM, CT, or coupon evidence.
Do not ask for titanium only as a material label. Ask for the titanium grade, delivered condition, exposed surfaces, and evidence package that match the process duty.
CP Titanium vs Ti-6Al-4V: Do Not Guess
Ti-6Al-4V is often the first AM quote route because it is widely available in LPBF supply chains, strong, and familiar to suppliers. Ti-6Al-4V ELI may be reviewed when ductility, fracture behavior, or a tighter acceptance basis matters. CP titanium may be more relevant when corrosion behavior, ductility, or chemical compatibility matters more than strength.
For battery recycling and critical minerals processing, the alloy question should come early because the wrong material assumption can invalidate a quote. A supplier who can print Ti-6Al-4V may not have a mature route for CP titanium. A buyer who needs CP titanium for corrosion testing should not accept a Ti-6Al-4V price as equivalent without review.
Choose the material based on:
- Acid, chloride, oxidizer, solvent, and cleaning chemistry.
- Temperature, pressure, solids, erosion, and stagnation.
- Whether the part is structural, flow-carrying, pressure-retaining, or only a coupon holder.
- Supplier process capability for the requested alloy.
- Post-processing, passivation, machining, coating, or finishing requirements.
- Documentation level: COA, COC, powder lot, heat-treatment record, build record, and inspection report.
Use Titanium AM Material Selection: Ti-6Al-4V, ELI, and CP Titanium when the alloy is not locked. Do not let every supplier quote a different titanium grade under the same corrosive service part number.
Black Mass and Solids Change the Design
Battery recycling hardware often deals with solids, not only clean liquids. Black mass, graphite, metal fines, precipitates, and filter cake can collect in dead legs, corners, surface texture, and low-flow regions. That changes the DfAM review.
High-risk features include:
- Blind flow paths with no powder exit or flushing route.
- Sharp internal shelves that collect black mass or precipitate.
- Fine lattice or mixer features that cannot be inspected or cleaned.
- Long dead legs near sample ports, pressure taps, or drain points.
- Small restrictions that can trap both AM powder and process solids.
- Thin walls between incompatible fluids or between process and ambient sides.
- Internal channels where roughness controls solids retention or pressure drop.
- Sealed cavities connected to wetted regions.
If the channel controls process performance, define depowdering, internal roughness, solids handling, flow test, pressure drop, cleaning, and CT assumptions before quoting. CT is useful when it answers a real question about trapped powder, blockage, wall thickness, or hidden defects, but it needs a defined feature size and acceptance scope.
Use Titanium 3D Printed Internal Channels: Powder Removal and CT before freezing a printed leach-loop manifold, mixer, nozzle, or process block.
Seal Faces and Ports Need Machining Stock
A printed titanium process body can combine ports, brackets, sampling points, pressure taps, and drain features. It should not rely on as-built AM surfaces for sealing or precision assembly.
Define every functional interface:
- O-ring grooves, gasket lands, flange faces, valve seats, and metal-seal surfaces.
- Pipe threads, tube fittings, bosses, bolt pads, dowel holes, and datum faces.
- Drain points, sample ports, pressure taps, vent ports, and cleaning ports.
- Surfaces that may remain as-built and surfaces that must be machined, polished, lapped, or finished.
- Mating materials, elastomers, liners, coatings, and fastener assumptions.
Add machining stock to seal faces, O-ring grooves, threaded ports, gasket lands, datum pads, and any surface that controls assembly. If a port intersects an internal AM channel, define how that transition will be cleaned and inspected.
For drawing and measurement strategy, use Titanium 3D Printing Tolerances: Datum Planning and CMM.
Leak Testing, Pressure Testing, and Cleaning
Battery recycling and critical minerals hardware can be under-tested or over-tested. A coupon rack may need simple documentation. A pilot leach-loop manifold with hidden channels may need CMM, CT, pressure testing, cleaning evidence, and material traceability.
Define:
- Working pressure, proof pressure, and pressure cycling if relevant.
- Test fluid or gas and whether it is compatible with the part condition.
- Allowable leakage, hold time, and test temperature.
- Whether testing happens before or after final machining, cleaning, passivation, or packaging.
- Which ports are capped and which are connected during testing.
- Whether testing covers each circuit separately or the full assembly.
- Whether flow, pressure drop, drainability, or cleaning verification is part of acceptance.
Weak wording:
Include leak testing.
Better wording:
Quote this titanium AM leach-loop manifold as delivered accepted hardware. The part carries acidic black mass leachate during pilot testing and includes six threaded ports, two sample ports, one drain point, and a machined gasket face. Please include alloy recommendation, machining stock, cleaning route, pressure-hold method, leak threshold and hold time, CMM for ports and datums, CT or flow-test recommendation for the internal channels, surface condition, and material traceability.
That wording gives the supplier a manufacturing and acceptance route, not only a printed shape.
Surface Finish, Passivation, and Residue Control
As-built titanium AM surfaces are not equivalent to machined, polished, lined, or molded surfaces. Roughness can trap powder, black mass, graphite, salt crystals, corrosion products, and cleaning residue. It can also affect pressure drop, solids carryover, seal behavior, and fatigue in pressure-cycled regions.
Separate surfaces by function:
- Seal faces, O-ring grooves, gasket lands, and valve seats.
- Threaded ports, fitting seats, sample ports, and pressure taps.
- Wetted channels where roughness affects solids retention, cleaning, or pressure drop.
- Mixer and nozzle surfaces where blockage or erosion matters.
- Fatigue or pressure-cycle surfaces where support scars are unacceptable.
- Datum pads and bolt faces that require CMM control.
- Noncritical exterior surfaces that may remain as-built or bead blasted.
Post-processing may include stress relief, HIP when justified, support removal, machining, abrasive flow finishing, chemical finishing, blasting, passivation, ultrasonic cleaning, drying, capping, and clean packaging. The sequence matters because a part can pass a pressure test and still be unacceptable if residue remains in a hidden path.
Use Post-Processing for Titanium 3D Printing when defining delivered condition.
Process Choice: LPBF Usually Leads for Compact Pilot Hardware
Review the proposed route against the solids and cross-contamination problem. Identify the black-mass or graphite stream, particle distribution, solids loading, sample representativeness, dead volumes, and cleaning between batches. Ask which internal surfaces can be finished and inspected and whether replaceable wear features are preferable to a consolidated body.
A process is not acceptable merely because it can print the flow path. If retained solids or cleaning residues cannot be evaluated, revise the geometry or compare a conventional assembly. Use the LPBF, EBM, and DED comparison for general manufacturing choices.
Inspection Evidence Should Match the Risk
The right inspection package depends on the part’s role. A coupon holder does not need the same evidence as a pressure-retaining acidic leach-loop manifold. A production-intent dosing nozzle may need more evidence than a one-day geometry trial.
Typical evidence includes:
- CMM report for ports, datums, seal faces, bolt patterns, gasket lands, and machined features.
- CT inspection for internal channels, trapped powder, wall thickness, hidden defects, or blockage where risk justifies it.
- Pressure, leak, flow, drainability, or pressure-drop test tied to the accepted configuration.
- Surface roughness checks on sealing, fatigue, or wetted-cleanability regions.
- Material certification, COA, COC, heat-treatment record, build record, powder lot, and traceability.
- Inspection photos for support removal, machined features, critical surfaces, and test setup.
- Coupon evidence when the lot, process, corrosion exposure, or acceptance basis requires it.
Use Titanium AM Qualification and Inspection Evidence to choose evidence by risk. A low quote with no test scope may simply omit the work needed to make the part acceptable.
Cost: Compare Delivered Process Hardware
Titanium AM can reduce fittings, shorten pilot-line iteration, and combine ports, mounts, and flow paths in one corrosion-resistant body. It can also hide cost in post-processing and evidence.
Cost drivers include:
- Manufacturability review and corrosion exposure review.
- Build orientation and support strategy.
- Support removal from ports, ribs, mixers, and internal openings.
- Stress relief, HIP if justified, and heat treatment.
- Machining of seal faces, threads, gasket lands, bores, and datum pads.
- Internal cleaning, flushing, drying, and residue verification.
- Passivation, polishing, abrasive flow finishing, or chemical finishing.
- CT, CMM, leak testing, pressure testing, flow testing, and roughness checks.
- Material records, lot traceability, inspection reports, and packaging.
- Rework if internal channels cannot be cleaned or verified.
Control cost before geometry is frozen. Remove unnecessary sealed cavities, keep process paths cleanable, machine only functional surfaces, define evidence by risk, and allow supplier DfAM changes before final pricing.
For quote normalization, use Titanium 3D Printing Cost Drivers: How to Reduce RFQ Price and the Titanium AM RFQ and Procurement Guide.
Better RFQ Wording
Weak RFQ:
Please quote this titanium 3D printed battery recycling part.
Better RFQ:
Please review this titanium AM manifold for a battery recycling pilot leach loop. The part carries acidic black mass slurry during short-duration test campaigns and includes four process ports, two sample ports, one drain point, and a machined gasket face. Please recommend Ti-6Al-4V, Ti-6Al-4V ELI, or CP titanium based on the exposure notes; identify powder-removal access, support strategy, machining stock, cleaning route, pressure-test method, leak threshold, CMM scope, CT or flow-test recommendation for the internal channels, material traceability, and any DfAM changes needed before quotation. Quote the delivered accepted part, not only the printed shape.
That wording helps procurement compare suppliers on the same route: print, stress relieve, depowder, machine, clean, inspect, test, document, and package.
Battery Recycling Titanium AM RFQ Checklist
Send the supplier:
- STEP file and drawing with datums, section views, and critical surfaces.
- Target alloy, material condition, and whether substitutions are allowed.
- Quantity, prototype or production intent, lot definition, and target lead time.
- Process step: leaching, separation, solvent extraction, purification, precipitation, washing, brine testing, or coupon exposure.
- Process media: black mass slurry, acid, base, chloride brine, sulfate solution, oxidizer, solvent, rinse water, solids loading, pH, temperature, pressure, and duty cycle.
- Mating materials, elastomers, coatings, liners, fasteners, and galvanic or compatibility assumptions.
- Working pressure, proof pressure, leak threshold, flow rate, pressure drop, drainability, and test method.
- Functional interfaces: seal faces, valve seats, O-ring grooves, gasket lands, threads, ports, sensor datums, and mounting pads.
- Internal channel details: minimum feature size, blind regions, powder-removal access, accepted roughness, flushing route, and cleanability.
- Post-processing expectations: stress relief, HIP if justified, machining, finishing, passivation, cleaning, drying, capping, and packaging.
- Inspection scope: CMM, CT, pressure test, leak test, flow test, roughness, coupons, COA, COC, build record, powder lot, and inspection photos.
- Permission for supplier DfAM changes before final pricing.
If the RFQ does not define exposure, solids, sealing, pressure, cleaning, and evidence, suppliers may quote very different products under the same part number.
When to Redesign or Avoid Titanium AM
Redesign before quotation when:
- Process paths have no practical powder exit, flushing path, or drain point.
- Black mass, precipitate, or graphite can collect in inaccessible dead zones.
- Seal faces, gasket lands, valve seats, or threaded ports lack machining stock.
- Internal roughness controls solids retention or pressure drop, but no finishing or flow-test route is defined.
- The part mixes incompatible fluids across thin walls with no inspection basis.
- CT cannot resolve the smallest critical internal feature.
- Pressure testing is required but pressure, method, hold time, and leakage limit are vague.
- CP titanium is required but the supplier route only supports Ti-6Al-4V.
- A simple machined or fabricated part would meet the requirement with lower acceptance risk.
Avoid titanium AM when standard polymer, fluoropolymer-lined steel, stainless, duplex stainless, nickel alloy, conventional titanium fabrication, machining, casting, or catalog process hardware meets the chemistry, cost, lead-time, and evidence requirements with lower risk.
Bottom Line
Titanium 3D printing can be valuable for battery recycling and critical minerals processing parts when it solves a real hardware problem: corrosion-resistant compact routing, fewer leak paths, low-volume pilot hardware, replacement of difficult drilling, integrated sampling and sensor ports, or documented internal-channel evidence. The strongest candidates are leach-loop manifolds, dosing nozzles, static mixers, pump and valve adapters, lithium brine test bodies, coupon racks, filter adapters, and process-development fixtures where exposure, sealing, machining, cleaning, and evidence are planned from the start.
The weak cases are simple shapes, commodity fittings, large fabricated equipment, high-volume standard parts, and any wetted or pressure path where the RFQ ignores alloy selection, powder removal, surface finish, solids handling, cleaning, leak testing, and traceability.
For an RFQ review, send CAD, drawing, process exposure map, pressure and leak requirement, target alloy, quantity, post-processing expectations, and inspection scope through the RFQ inputs page or email info@szcomo.com.
- Battery recycling
- Critical minerals
- Hydrometallurgy
- Black mass
- Lithium
- Corrosion
- CP titanium
- Leak testing
- RFQ