· Updated - TITANIUM 3DP Engineering - Engineering Guides - 15 min read
Titanium 3D Printing for Chemical Processing and Water Treatment Parts
Engineering RFQ guide for titanium 3D printed chemical processing and water treatment parts, covering corrosion exposure, CP titanium vs Ti-6Al-4V, pump and valve bodies, manifolds, static mixers, leak testing, CT, CMM, and traceability.
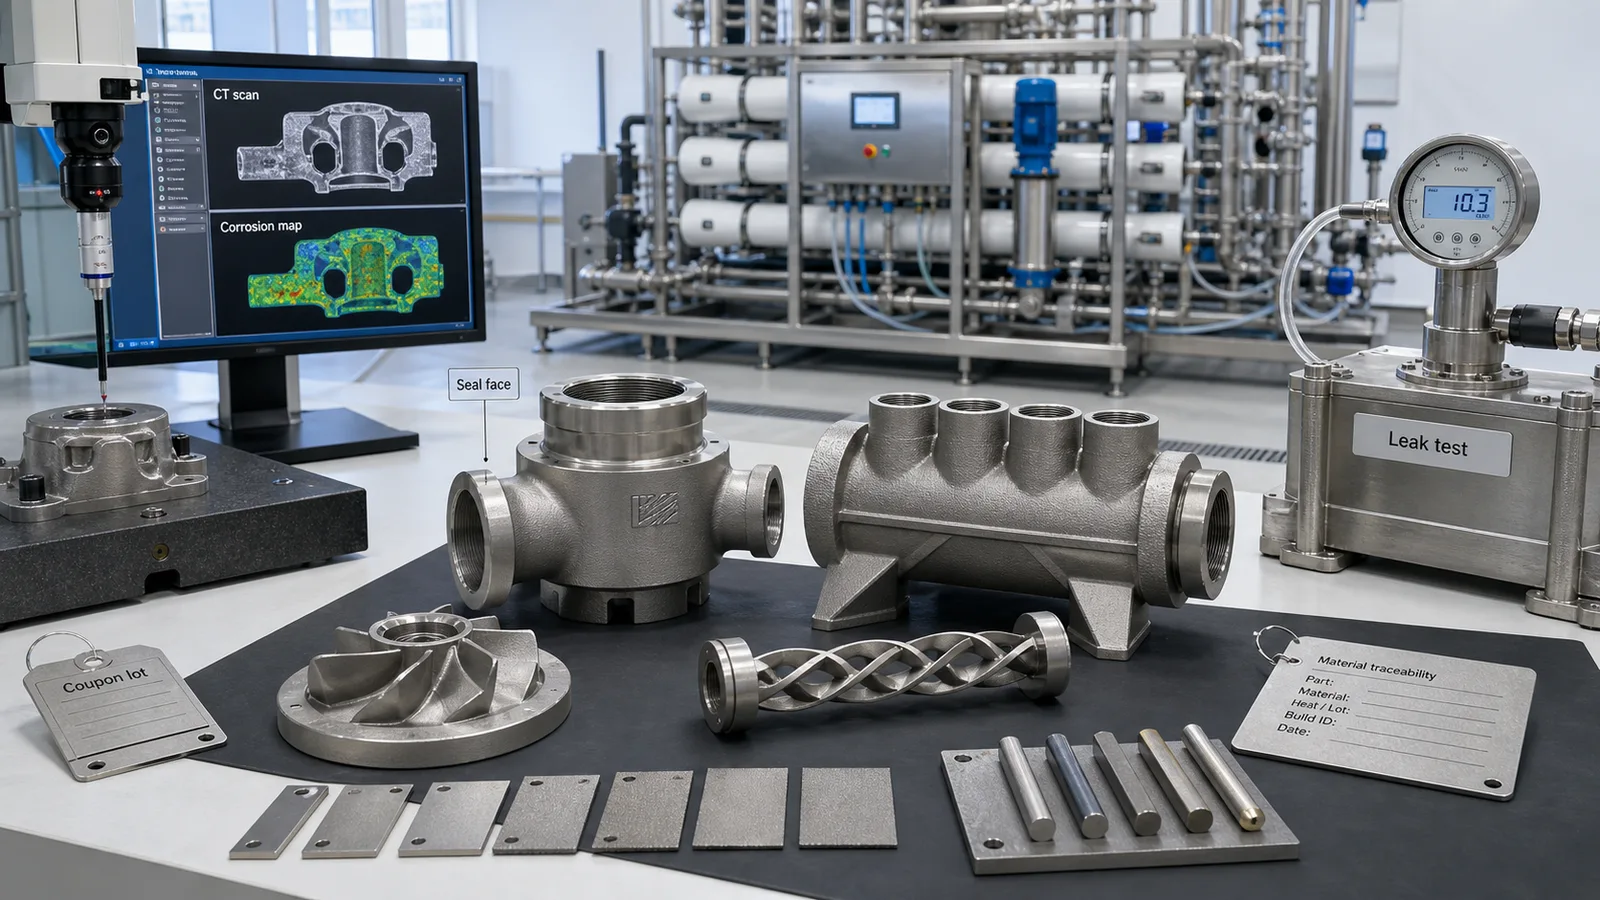
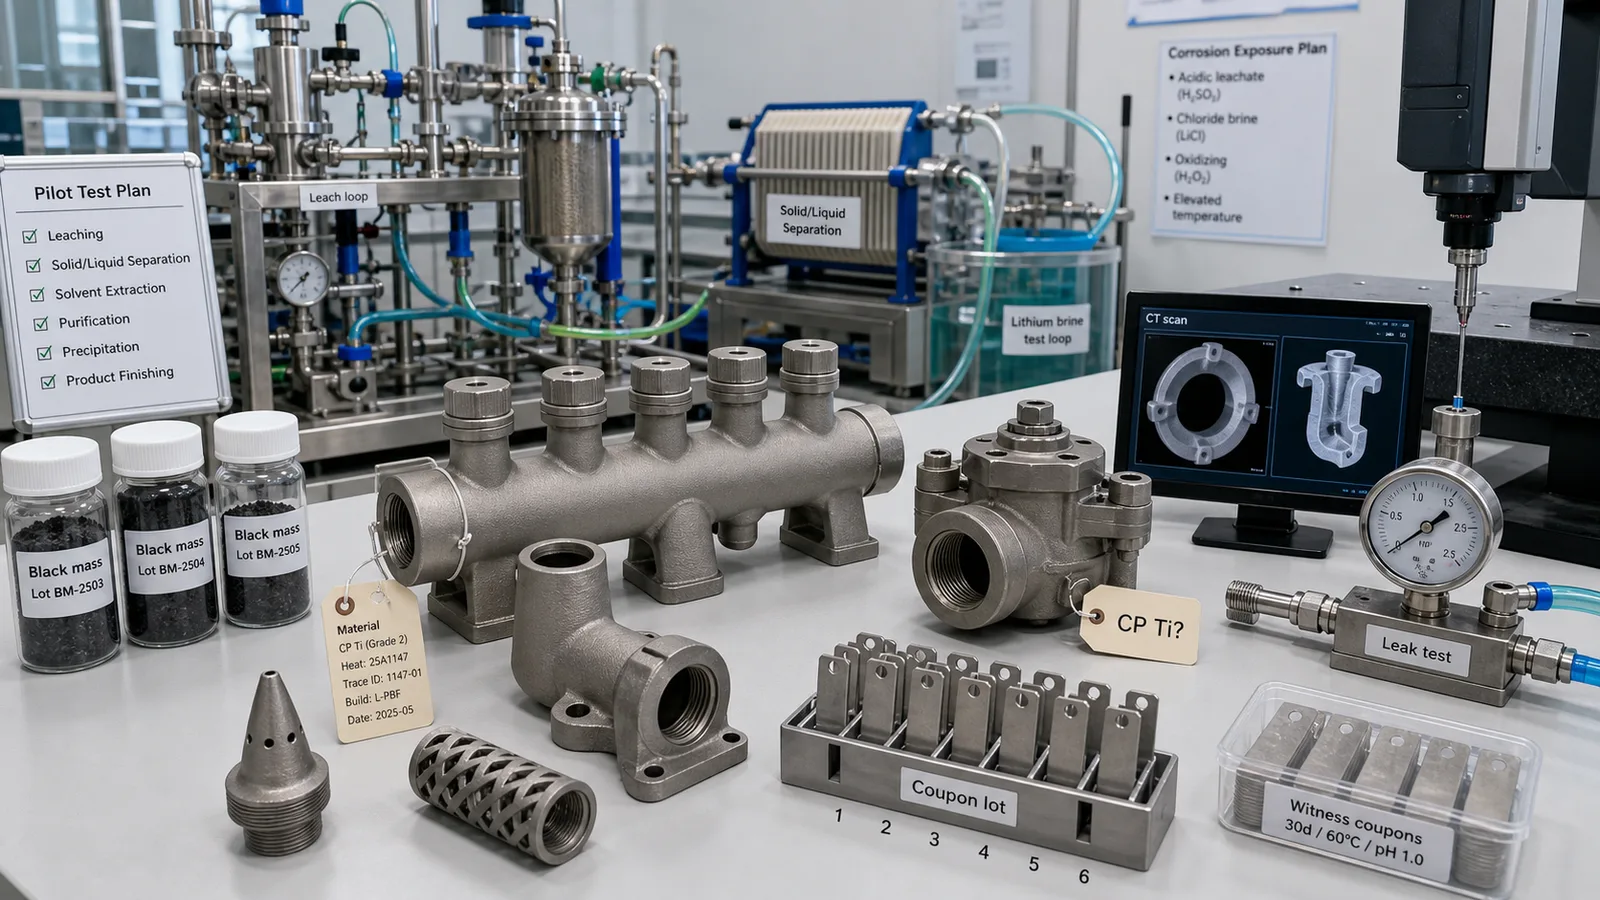
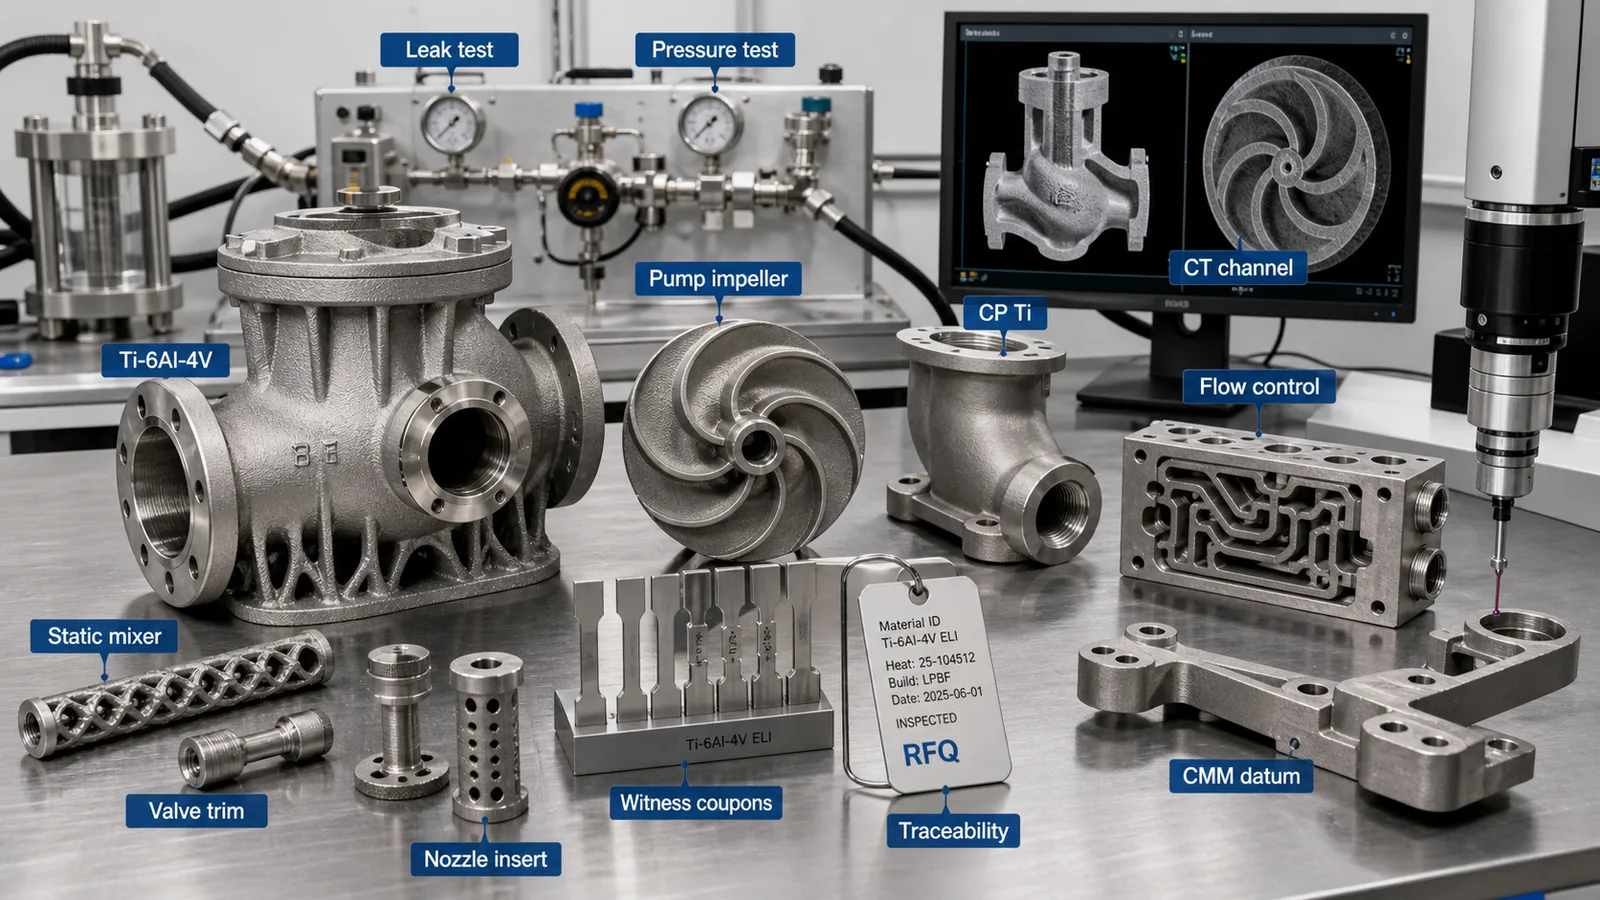
Representative article image; not a customer acceptance record or proof of a qualified manufacturing route. Refer to the cited sources and part-specific inspection records for engineering evidence.
On this page
Titanium 3D printing for chemical processing and water treatment parts is useful when corrosion exposure, compact fluid routing, low-volume replacement, fewer leak paths, or difficult machining creates a real engineering advantage. It is not a shortcut around chemical compatibility, pressure testing, cleaning, or plant acceptance.
The best RFQs treat a printed titanium valve body, process manifold, pump adapter, static mixer, sample block, sensor port, nozzle, or corrosion coupon fixture as delivered process hardware. That means the quote must cover alloy selection, exposure mapping, seal faces, internal cleaning, pressure or leak testing, CMM, CT when hidden passages matter, material records, and traceability.
For a broad application map, start with Titanium 3D Printing Applications and use this guide for chemical-processing and water-treatment-specific decisions. For the cross-industry valve, pump, static mixer, nozzle, and flow-control sourcing route, use Titanium 3D Printing for Industrial Valves, Pump Parts, and Flow Control Hardware. For seawater RO, brine concentration, and MLD/ZLD pilot hardware, use Titanium 3D Printing for Seawater Desalination and Brine Concentration Hardware. For lithium brine, DLE pilot skids, and critical-minerals brine hardware, use Titanium 3D Printing for Direct Lithium Extraction and Brine Processing Hardware.
For refinery, LNG, produced-water, petrochemical, and oilfield process hardware where API 20S, sour-service review, pressure testing, and operator acceptance may enter the RFQ, use Titanium 3D Printing for Oil & Gas, LNG, and Petrochemical Hardware. For mining, mineral processing, acid leach, slurry, flotation, tailings-water, and hydrometallurgy pilot hardware, use Titanium 3D Printing for Mining, Mineral Processing, and Hydrometallurgy Hardware.
Quick Answer
Titanium additive manufacturing is worth reviewing for chemical and water-treatment equipment when the part is compact, corrosion-exposed, interface-heavy, low-volume, or functionally improved by internal geometry.
Good candidates include:
- Compact pump impellers, pump adapters, seal carriers, and wear-ring trial parts for corrosive service.
- Valve bodies, valve trim prototypes, bypass blocks, and instrument manifolds with multiple ports.
- Static mixers, dosing nozzles, chemical-injection bodies, sample ports, and sensor housings.
- Reverse-osmosis, nanofiltration, desalination, brackish-water, or industrial-water pilot hardware.
- Corrosion test fixtures, coupon racks, and process-development parts where titanium exposure data matters.
- Heat-transfer or process-flow bodies that combine corrosion resistance with internal channels.
- Low-volume spares where a machined or fabricated route is slow and the geometry benefits from AM.
Weak candidates include simple plates, pipe spools, commodity fittings, large tanks, high-volume cast parts, and any pressure or chemical-contact part where the RFQ does not define fluid chemistry, temperature, concentration, cleaning route, seal faces, proof test, and documentation.
If the part can be made from standard pipe, tube, plate, billet, polymer, fluoropolymer-lined hardware, stainless steel, duplex stainless, nickel alloy, or conventional fabrication with lower risk, use the When Not to Use Titanium Additive Manufacturing screen before requesting production pricing.
Why This Topic Is Timely in 2026
Chemical and water-treatment hardware is getting more attention because the process environment is changing faster than standard catalog hardware can always support. PFAS treatment, brackish groundwater use, water reuse, compact pilot plants, distributed treatment skids, and industrial water reliability all push engineers toward smaller documented components with better corrosion assumptions.
Recent public signals are useful context:
- The EPA Drinking Water Treatability Database covers referenced treatment information for regulated and unregulated contaminants, including PFAS, and is built for utilities, designers, agencies, and researchers.
- EPA’s overview of drinking water treatment technologies keeps granular activated carbon, ion exchange, reverse osmosis, and nanofiltration in the practical treatment conversation for several contaminants, including PFAS.
- The USGS National Brackish Groundwater Assessment notes that industry and public drinking-water suppliers are increasingly turning to brackish groundwater, often using reverse osmosis or other desalination processes when lower dissolved solids are needed.
- The Bureau of Reclamation’s Brackish Groundwater National Desalination Research Facility exists specifically to develop technologies for desalination of brackish and impaired groundwater in inland states.
- DOE has continued to fund desalination and water reuse work through the National Alliance for Water Innovation, including a 2024 announcement of $75 million in renewed funding.
- A 2026 study in npj Materials Degradation compared corrosion resistance of Ti-6Al-4V made by different additive routes and reinforced a practical point for buyers: process route, surface condition, porosity, and microstructure are not cosmetic details.
These signals do not mean every water-treatment or chemical-processing part should be printed in titanium. They do explain why buyers are asking sharper RFQ questions about corrosion exposure, internal cleanliness, leak paths, delivered testing, and documented material condition.
Where Titanium AM Fits in Process Equipment
Titanium is not selected only because it resists corrosion. It earns a review when its corrosion behavior, strength-to-weight ratio, low magnetic response, heat tolerance, or additive geometry improves the delivered process system.
| Part family | Why titanium AM can help | Main RFQ risk | Evidence to define |
|---|---|---|---|
| Pump adapter or impeller trial part | Compact wetted geometry and fast iteration | Surface finish, balance, and erosion | Machining plan, roughness, runout, test duty |
| Valve body or valve trim prototype | Integrated ports, compact routing, low-volume geometry | Seal leakage and crevice corrosion | Machined seal faces, pressure/leak test, CMM |
| Chemical manifold or dosing block | Fewer fittings, fewer plugs, shorter fluid paths | Powder removal and hidden residue | CT or flow check, cleaning route, pressure test |
| Static mixer or process nozzle | Internal geometry that is hard to machine | Blockage, roughness, and cleanability | Flow test, depowdering plan, accepted roughness |
| Sensor, sample, or instrument body | Integrated ports and datum features | Thread quality and sealing | Machined threads, datum plan, leak threshold |
| Desalination or RO pilot hardware | Corrosion-resistant low-volume test components | Chloride, brine, and cleaning compatibility | Exposure map, alloy review, material records |
| Corrosion coupon fixture | Matched titanium exposure hardware | Over-specifying a simple holder | Alloy, surface condition, coupon lot records |
The strongest cases are not generic “chemical parts.” They are compact wetted components where additive manufacturing reduces leak paths, replaces drilled cross-holes, integrates ports, improves pilot-line iteration, or makes a cleanable flow path possible.
For thermal process equipment, use Titanium 3D Printed Heat Exchangers. For seawater-specific hardware, use Titanium 3D Printing for Marine, Subsea, and Offshore Parts. For hydrogen or PEM water-loop hardware, use Titanium 3D Printing for Hydrogen Electrolyzer and Fuel Cell Parts.
Start With a Corrosion Exposure Map
“Chemical resistant” is not an RFQ requirement. A useful quote needs a corrosion exposure map. Without it, suppliers may price the same part as a prototype shape, a low-risk utility component, or a documented process-wetted component.
Define:
- Process fluid, byproduct, wash fluid, and cleaning chemistry.
- Concentration, pH, dissolved oxygen, chloride level, solids, and contaminants if known.
- Temperature, pressure, flow rate, stagnation periods, and duty cycle.
- Whether the part sees continuous immersion, spray, vapor, condensation, or intermittent wetting.
- Whether crevices, dead legs, gasket pockets, and trapped liquid regions are acceptable.
- Mating metals, fasteners, elastomers, coatings, liners, and electrical contact.
- Whether the part is structural, flow-carrying, pressure-retaining, or only a test fixture.
- Acceptance tests: leak, pressure hold, flow, cleaning verification, roughness, CMM, CT, or coupon evidence.
Do not ask for titanium only as a material label. Ask for the titanium grade, delivered condition, exposed surfaces, and evidence package that match the process duty.
CP Titanium vs Ti-6Al-4V: Do Not Guess the Alloy
Ti-6Al-4V is often the first AM quote route because it is widely available in LPBF supply chains and is covered by standards such as ASTM F2924 for powder-bed-fusion Ti-6Al-4V components. Ti-6Al-4V ELI may be reviewed when the project needs extra-low-interstitial control or a specific acceptance basis; ASTM F3001 covers powder-bed-fusion Ti-6Al-4V ELI components.
Commercially pure titanium is a different discussion. CP titanium may be more relevant when corrosion behavior, ductility, or chemical compatibility matters more than high strength. It may also be harder to source through a given AM supplier route, so it should be reviewed early rather than added after pricing.
If the drawing or search brief uses Grade 2, TA2, TA2G, or generic CP titanium language, use the commercially pure titanium AM sourcing guide before accepting a supplier’s proposed equivalence or Ti-6Al-4V substitution.
Choose the material based on:
- Chemical service, concentration, temperature, and cleaning chemistry.
- Strength, pressure, fatigue, and stiffness requirements.
- Whether the part is a prototype, pilot-plant component, or production-intent part.
- Supplier availability for LPBF, EBM, or another route in the requested grade.
- Post-processing, passivation, machining, coating, or finishing requirements.
- Certification package: COA, COC, powder lot, heat-treatment record, build record, and inspection report.
The broader alloy framework is in Titanium AM Material Selection: Ti-6Al-4V, ELI, and CP Titanium. The important point for process equipment is simple: do not let three suppliers quote three different titanium grades under one corrosion-risk part number.
Pump, Valve, and Manifold Parts Need Seal Planning
Many process-equipment RFQs fail because the CAD model shows the flow body but not the seal strategy. AM can create compact porting, organic transitions, and fewer fittings, but as-built AM surfaces are not seal faces.
Define every functional interface:
- O-ring grooves, gasket lands, flange faces, valve seats, and metal-seal surfaces.
- Pipe threads, tube fittings, bosses, bolt pads, dowel holes, and datum faces.
- Shaft bores, impeller interfaces, wear-ring regions, and bearing-adjacent surfaces.
- Drain points, sample ports, pressure taps, and cleaning ports.
- Surfaces that may remain as-built and surfaces that must be machined, polished, lapped, or finished.
Add machining stock where seals, threads, ports, and datums matter. If a port intersects an internal AM channel, define how the transition will be cleaned and inspected. If the part uses an elastomer, identify the chemistry and temperature. If it uses a metal gasket, define surface finish and flatness expectations.
For drawing strategy, use Titanium 3D Printing Tolerances: Datum Planning and CMM before sending a quote package.
Internal Channels and Static Mixers Are Useful but Easy to Underquote
Internal geometry is one of the strongest reasons to print process hardware. It can replace drilled cross-holes, plugs, welded bosses, external tubes, and stacked plates. It can also trap powder, cleaning media, corrosion products, or process residue if the geometry is not designed for acceptance.
High-risk features include:
- Blind chemical paths with no powder exit or flushing route.
- Small restrictions that partially sintered powder can block.
- Sharp internal shelves where solids, scale, or cleaning residue can collect.
- Static-mixer elements that cannot be inspected or flow-tested.
- Parallel paths with no pressure-drop or flow-balance check.
- Thin walls between incompatible fluids or between process and ambient sides.
- Sealed lattice structures inside wetted regions.
- Long dead legs near sample ports, pressure taps, or drain points.
If a channel controls process performance, include depowdering, cleaning, internal roughness, pressure drop, and inspection assumptions in the RFQ. CT is useful when it answers a real question about blockage, wall thickness, trapped powder, or hidden defects, but it needs a defined feature size and acceptance scope.
Use Titanium 3D Printed Internal Channels: Powder Removal and CT before freezing a printed manifold, mixer, nozzle, or compact dosing block.
Pressure, Leak, and Flow Testing
Chemical and water-treatment parts often combine corrosion exposure with pressure or leak requirements. Do not accept a printed titanium flow body only because it looks dense. The test method should match the failure mode and the actual process duty.
Define:
- Working pressure, proof pressure, burst requirement if any, and pressure cycling.
- Test fluid or gas, temperature during test, and whether the test medium is compatible with the part.
- Leak-test method, allowable leakage, hold time, port sealing method, and fixture responsibility.
- Whether pressure testing happens before or after machining, finishing, cleaning, or passivation.
- Whether both sides of a multi-circuit part are tested separately.
- Flow rate, pressure drop, and flow-balance requirements if channel openness affects performance.
- Whether test results are development data, shipment acceptance, or qualification evidence.
Weak wording:
Include leak testing.
Better wording:
Quote this titanium AM dosing manifold as delivered accepted hardware. The part carries 6 bar process water with intermittent acidic cleaning. Please include final machining of seal faces and threads, cleaning after machining, pressure hold at the agreed proof pressure, leak threshold and hold time, CMM for ports and datums, and CT or flow-test recommendation for the two internal channels.
That wording gives the supplier a real acceptance target instead of a test label.
Surface Finish, Cleaning, and Residue Control
As-built titanium AM texture can be acceptable on noncritical exterior surfaces. It can be wrong for seal faces, gasket lands, threaded ports, fatigue-sensitive edges, sliding interfaces, or wetted regions that must be cleaned repeatedly.
Separate surfaces by function:
- Seal faces, O-ring grooves, gasket lands, valve seats, and lapped interfaces.
- Threaded ports, tube-fitting seats, and pressure-tap interfaces.
- Wetted internal channels where roughness affects residue, pressure drop, or cleaning.
- Pump or nozzle surfaces where erosion, cavitation, or balance matters.
- Fatigue or pressure-cycle surfaces where support scars are unacceptable.
- Datum pads and bolt faces that require CMM control.
- Noncritical exterior areas that may remain as-built or bead blasted.
Post-processing may include stress relief, HIP when justified, support removal, machining, abrasive flow finishing, chemical finishing, blasting, passivation, ultrasonic cleaning, drying, packaging, and inspection photos. The right sequence matters because a part can pass a pressure test and still be unacceptable if cleaning residue remains in a hidden chemical path.
Use Post-Processing for Titanium 3D Printing when defining delivered condition.
Process Choice: LPBF Usually Leads for Compact Flow Parts
Choose the manufacturing route only after the exposure map is defined. For a process-wetted body, ask the supplier to identify which internal surfaces can be finished and cleaned, which sealing interfaces will be machined, and how the proposed material condition will be evaluated in the actual medium. A corrosion result from a different chemistry or surface condition is not a release basis.
Use the process comparison for LPBF, EBM, and DED trade-offs. Keep this page focused on chemical exposure; use the desalination guide for concentration and cleaning cycles and the DLE guide for sorbent and regenerant interfaces.
Inspection Evidence Should Match the Process Risk
Process-equipment parts can be under-tested or over-tested. A coupon rack does not need the same evidence as a pressure-retaining chemical manifold. A compact brine manifold with hidden channels may need CT, pressure testing, and CMM. A low-risk pilot-plant bracket may only need material records and a dimensional check.
Typical evidence includes:
- CMM report for ports, datums, seal faces, bolt patterns, gasket lands, and machined features.
- CT inspection for internal channels, trapped powder, wall thickness, hidden defects, or blockage where risk justifies it.
- Pressure, leak, flow, or pressure-drop test tied to the accepted configuration.
- Surface roughness checks on sealing, fatigue, or wetted-cleanability regions.
- Material certification, COA, COC, heat-treatment record, build record, powder lot, and traceability.
- Inspection photos for support removal, machined features, critical surfaces, and test setup.
- Coupon evidence when the lot, process, or acceptance basis requires it.
Use Titanium AM Qualification and Inspection Evidence to select evidence by part risk. A cheap quote with no test scope is often a print-only quote, not a delivered process-hardware quote.
Cost: Compare Delivered Process Hardware
Titanium AM can reduce fittings, shorten pilot-plant iteration, consolidate ports, and eliminate difficult drilling. It can also hide cost in post-processing and evidence.
Cost drivers include:
- Build orientation and support strategy.
- Support removal from ports, ribs, mixer elements, and internal openings.
- Stress relief, HIP if justified, and heat treatment.
- Machining of seal faces, valve seats, threads, gasket lands, bores, and datum pads.
- Internal cleaning, flushing, drying, and residue verification.
- Passivation, polishing, abrasive flow finishing, or chemical finishing.
- CT, CMM, leak testing, pressure testing, flow testing, and roughness checks.
- Material records, lot traceability, inspection reports, and packaging.
- Rework if internal channels cannot be cleaned or verified.
Control cost before geometry is frozen. Remove unnecessary sealed cavities, keep chemical paths cleanable, machine only functional surfaces, define evidence by risk, and let suppliers suggest DfAM changes before final pricing.
For quote normalization, use Titanium 3D Printing Cost Drivers: How to Reduce RFQ Price and the Titanium AM RFQ and Procurement Guide.
Better RFQ Wording
Weak RFQ:
Please quote this titanium 3D printed chemical manifold.
Better RFQ:
Please review this titanium AM flow manifold for a water-treatment pilot skid. The part carries process water and periodic cleaning solution, with four threaded ports, two sensor ports, one drain point, and a machined gasket face. Please recommend Ti-6Al-4V, Ti-6Al-4V ELI, or CP titanium based on the exposure notes; identify powder-removal access, support strategy, machining stock, cleaning route, pressure-test method, leak threshold, CMM scope, CT or flow-test recommendation for the internal channels, material traceability, and any DfAM changes needed before quotation. Quote the delivered accepted part, not only the printed shape.
That wording helps procurement compare suppliers on the same delivered route: print, stress relieve, depowder, machine, clean, inspect, test, document, and package.
Chemical and Water-Treatment Titanium AM RFQ Checklist
Send the supplier:
- STEP file and drawing with datums, section views, and critical surfaces.
- Target alloy, material condition, and whether substitutions are allowed.
- Quantity, prototype or production intent, lot definition, and target lead time.
- Process fluid, wash fluid, cleaning chemistry, concentration, pH, chlorides, temperature, pressure, and duty cycle.
- Mating materials, elastomers, coatings, liners, fasteners, and electrical contact assumptions.
- Working pressure, proof pressure, leak threshold, flow rate, pressure drop, and test method.
- Functional interfaces: seal faces, valve seats, O-ring grooves, gasket lands, threads, ports, sensor datums, and mounting pads.
- Internal channel details: minimum feature size, blind regions, powder-removal access, accepted roughness, flushing route, and drainability.
- Post-processing expectations: stress relief, HIP if justified, machining, finishing, passivation, cleaning, drying, and packaging.
- Inspection scope: CMM, CT, pressure test, leak test, flow test, roughness, coupons, COA, COC, build record, powder lot, and inspection photos.
- Permission for supplier DfAM changes before final pricing.
If the RFQ does not define exposure, sealing, pressure, cleaning, and evidence, suppliers may quote very different products under the same part number.
When to Redesign or Avoid Titanium AM
Redesign before quotation when:
- Chemical paths have no practical powder exit, flushing path, or drain point.
- Seal faces, gasket lands, valve seats, or threaded ports lack machining stock.
- Internal roughness controls cleaning or pressure drop, but no finishing or flow-test route is defined.
- The part mixes incompatible fluids across thin walls with no inspection basis.
- CT cannot resolve the smallest critical internal feature.
- Pressure testing is required but pressure, method, hold time, and leakage limit are vague.
- CP titanium is required but the supplier route only supports Ti-6Al-4V.
- A simple machined or fabricated part would meet the requirement with lower acceptance risk.
Avoid titanium AM when standard polymer, lined steel, stainless, duplex stainless, nickel alloy, conventional titanium fabrication, machining, or casting meets the chemistry, cost, lead-time, and evidence requirements with lower risk.
Bottom Line
Titanium 3D printing can be valuable for chemical processing and water treatment parts when it solves a real hardware problem: corrosion-resistant compact routing, fewer leak paths, low-volume pilot hardware, replacement of difficult drilling, integrated ports, or documented test components. The strongest candidates are pump and valve components, dosing manifolds, static mixers, sample blocks, sensor bodies, corrosion coupon fixtures, and water-treatment pilot parts where exposure, sealing, machining, cleaning, and evidence are planned from the start.
The weak cases are simple shapes, commodity fittings, large fabricated equipment, high-volume cast parts, and any wetted or pressure path where the RFQ ignores alloy selection, powder removal, surface finish, cleaning, leak testing, and traceability.
For an RFQ review, send CAD, drawing, exposure map, pressure and leak requirement, target alloy, quantity, post-processing expectations, and inspection scope through the RFQ inputs page or email info@szcomo.com.
- Chemical processing
- Water treatment
- Desalination
- Corrosion
- Pump parts
- Valves
- CP titanium
- Leak testing
- RFQ